Machine angled and multi-face features with fewer datum transfers
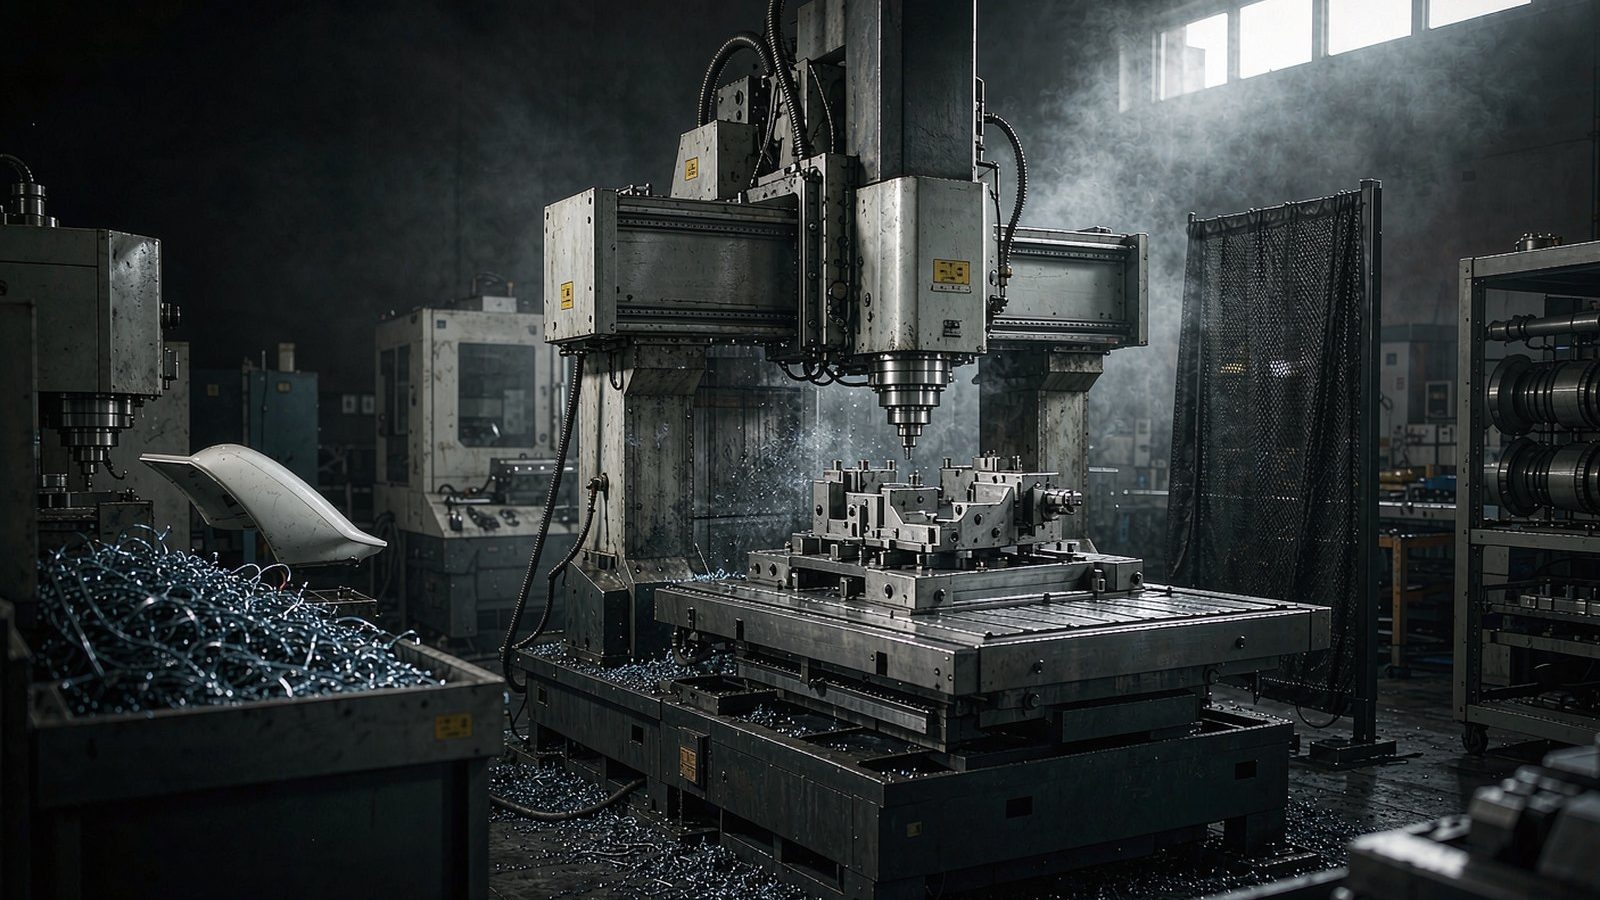
Multi-face precision machining
5-Axis CNC Machining
Cut down on repeated setups and reach angled, contoured and multi-face features with a process chosen from the drawing.
15 years
manufacturing experience
85+
machining & inspection systems
3/4/5-axis
milling, turning & turn-mill
Worldwide
B2B engineering support
Built around the buyer's requirement
From a complete RFQ to a controlled supply process.
Improve tool access to complex pockets, contours and interfaces
Validate difficult geometry through prototype and first-article inspection
Establish a repeatable route for low-volume and recurring orders
01
When 5-axis machining adds value
Five-axis work earns its place when critical features sit on several faces, at compound angles, or where conventional setups cannot reach without repeated re-clamping. Completing related operations in one orientation removes handling and datum-transfer risk.
Five-axis equipment is not automatically right for every part. We compare 3-axis, indexed 4-axis, simultaneous or positional 5-axis, turning and secondary operations against feature access, rigidity, tolerance and quantity before recommending a route.
- Angled bores, faces and mounting interfaces
- Complex pockets and multi-level geometry
- Contoured surfaces and restricted tool access
- Parts that gain from fewer repeated setups
02
Process planning for complex geometry
A sound sequence establishes reliable datums, preserves support during roughing and reserves controlled finishing operations for critical surfaces. Tool length, holder clearance, machine travel, collision risk and chip evacuation are reviewed before cutting starts.
Workholding must provide access without letting the component move under cutting forces. Prototype fixtures can stay flexible, while repeat production moves to soft jaws, fixture plates or dedicated supports tied to approved setup instructions.
03
Inspection based on functional relationships
Inspection concentrates on the dimensions and relationships the drawing defines: feature position, bore and hole geometry, profile, mating faces and functional datums. CMM inspection, gauges and conventional measurement can be combined under the agreed quality plan.
Customers should identify first-article reporting, selected dimensional results, revision control and material or finishing documentation at quotation stage so that inspection scope matches supplier approval requirements.
Prototype to production
A practical B2B manufacturing path
Every stage remains connected to the customer's approved drawing, revision and purchasing requirements.
-
01
Geometry review
Identify angled features, access limits, datums and tolerance relationships.
-
02
Setup strategy
Select 3/4/5-axis operations, tools and workholding for stable access.
-
03
Machining validation
Confirm toolpaths, feature relationships and edge condition on samples.
-
04
Production control
Maintain approved programs, setup references and inspection routines.
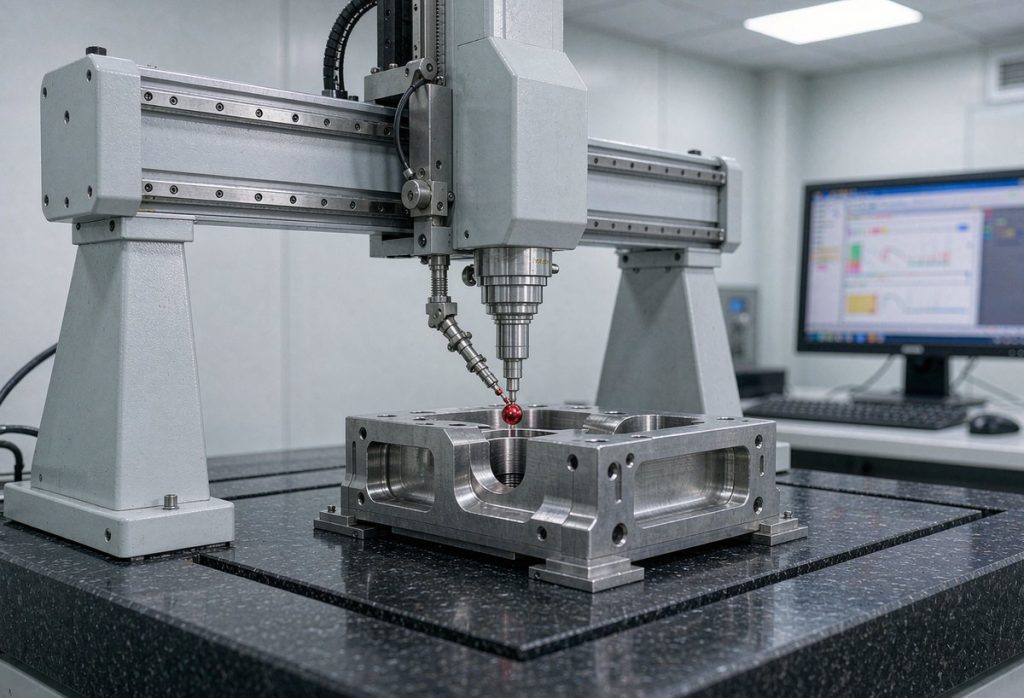
Inspection scope defined before production
Quality evidence for supplier approval
Measurement methods and documentation are selected from the released drawing and agreed purchase-order requirements.
- Datum-to-feature positional relationships
- Angled bores, faces and compound geometry
- Profile and mating-surface requirements
- Thread, edge and deburring condition
- First-article and repeat-batch consistency
Engineering and procurement FAQ
Answers before you request a quote
Does every complex part need 5-axis machining?
No. Indexed 4-axis, 3-axis with secondary setups or turn-mill work can be more practical. The route should follow geometry, tolerance and quantity.
What is needed for a 5-axis quotation?
The 3D model, 2D drawing, material, quantities, critical tolerances, finish, inspection scope and delivery requirements.
Can five-axis parts move into repeat orders?
Yes. Prototype validation confirms machining access, workholding and inspection before controlled programs and fixtures support repeat production.
How is collision risk managed?
Holder clearance, machine travel and fixture position are checked in the CAM environment and confirmed on the first part.
Start with complete project data
Send your drawings for engineering review.
Include STEP files, 2D drawings, material, quantities, tolerances, finish, inspection and delivery requirements.